Raw Material Inspection
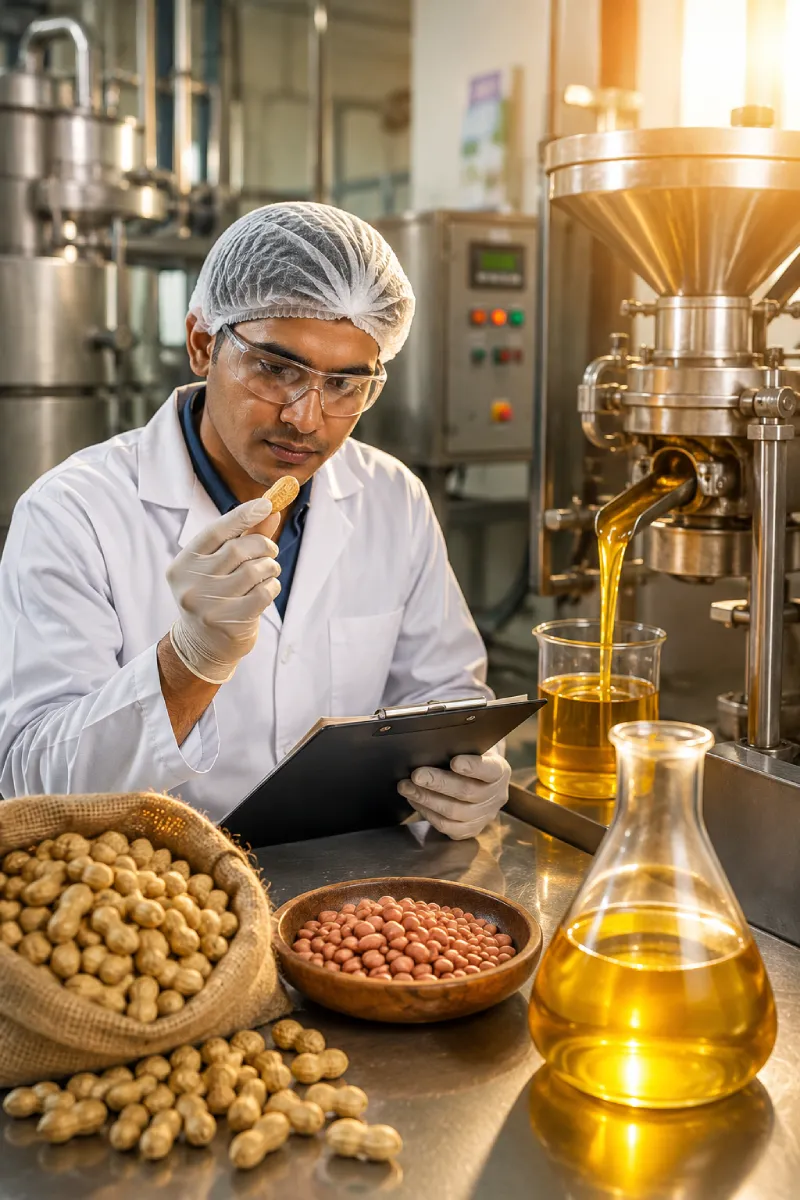
Every lot is checked for moisture, foreign matter and kernel quality before processing.
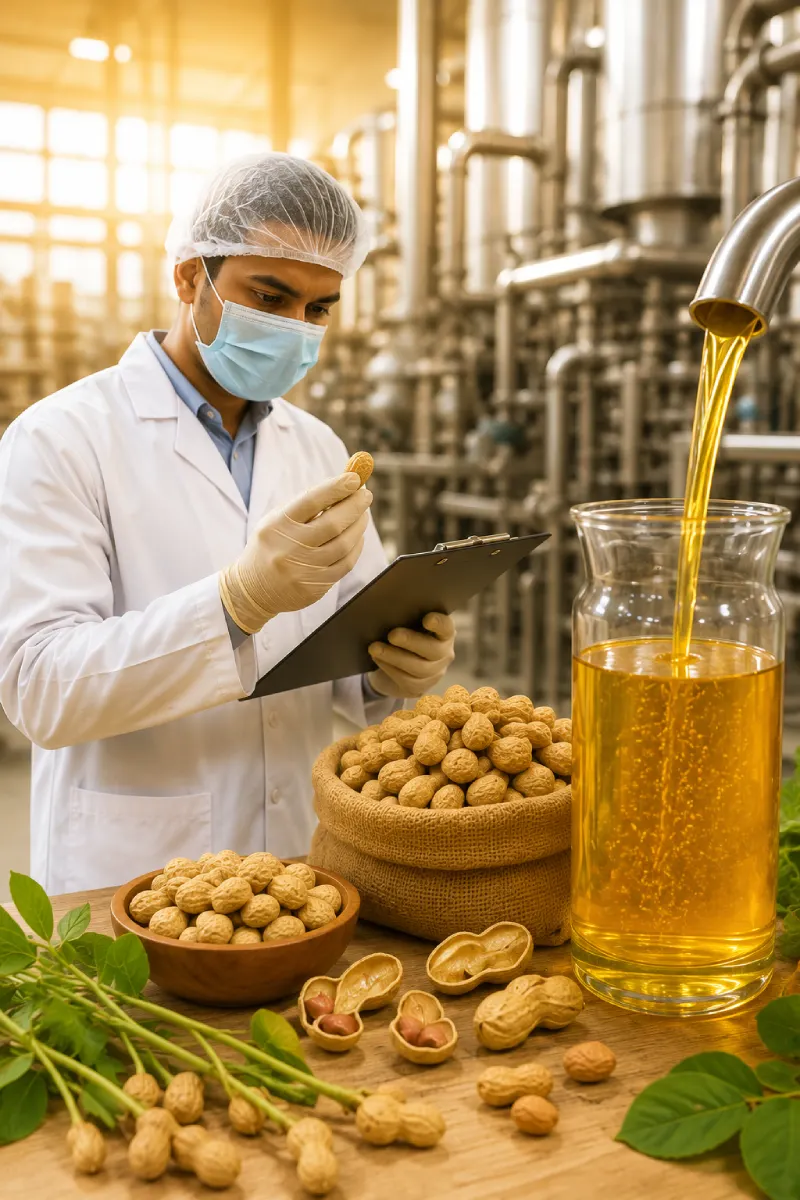
Quality control at Nilkanth starts long before the oil is pressed. Our team inspects every groundnut lot for size, moisture, mould and aflatoxin risk. Only kernels that pass our raw-material standards enter the production line.
During processing we monitor temperature, pressure and extraction time in real time. Our cold-press mechanical system never uses chemical solvents, so the natural aroma, colour and nutrients of the groundnut stay intact.
Every lot is checked for moisture, foreign matter and kernel quality before processing.
Pressing temperature, filtration pressure and flow are tracked at every stage.
Bottles and jars are inspected, sealed and batch-coded for complete traceability.
Our quality assurance team verifies that every batch meets the food safety and sensory standards your family deserves. We test for free fatty acids, moisture, peroxide value and purity before any product leaves the facility.
Each batch carries a unique code that links back to its raw material source, production date and laboratory report — so traceability is never a question.
Representative samples from every batch are taken for physical and chemical testing.
FFA, peroxide value, moisture and sensory profile are tested against internal limits.
Only batches that pass every test receive a batch release and are dispatched.
Our in-house checks and third-party lab verifications follow accepted food-oil standards, giving you confidence in every pack.
Free fatty acid levels are monitored to guarantee freshness and shelf stability.
Tests oxidation levels so the oil retains its natural aroma and nutritional value.
Controlled moisture keeps the oil clear, safe and free from microbial growth.
Every jar is coded so its origin, production date and test report can be traced.
We are committed to maintaining the highest standards of quality, safety, and excellence through recognized certifications and industry associations.